Skip to content
Synafloat
Book a call
In a call we clarify whether the simulation answers your parameter question.

Simulation software for laser DED with wire or powder

Parameters for six applications

The software adjusts laser power, travel speed and material feed layer by layer and writes them into your machine file.

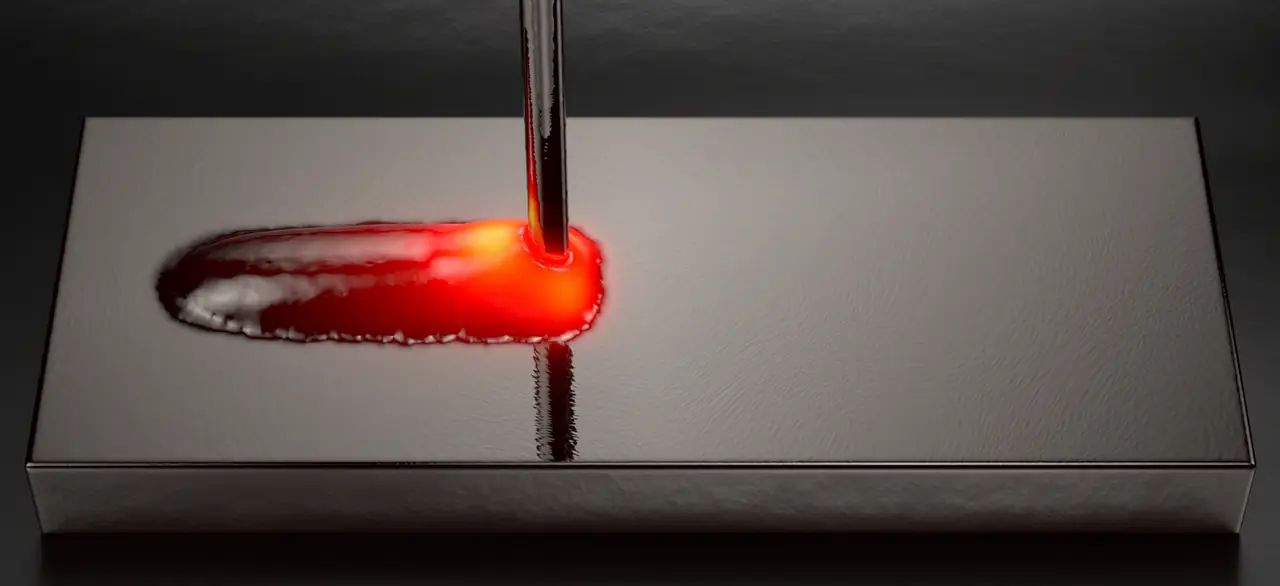
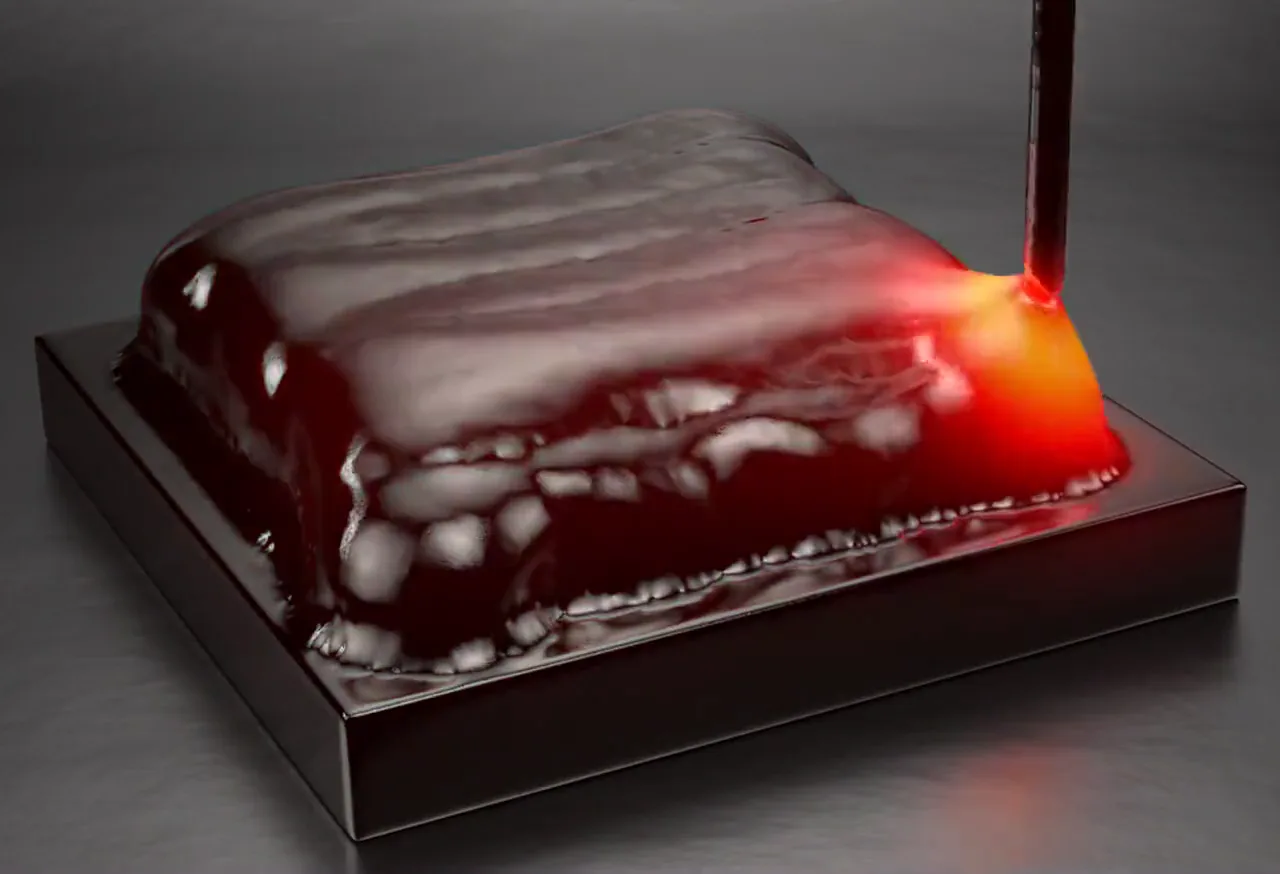
  1. New partRunCalibrated only with a measured bead

    Simulation, demonstrator

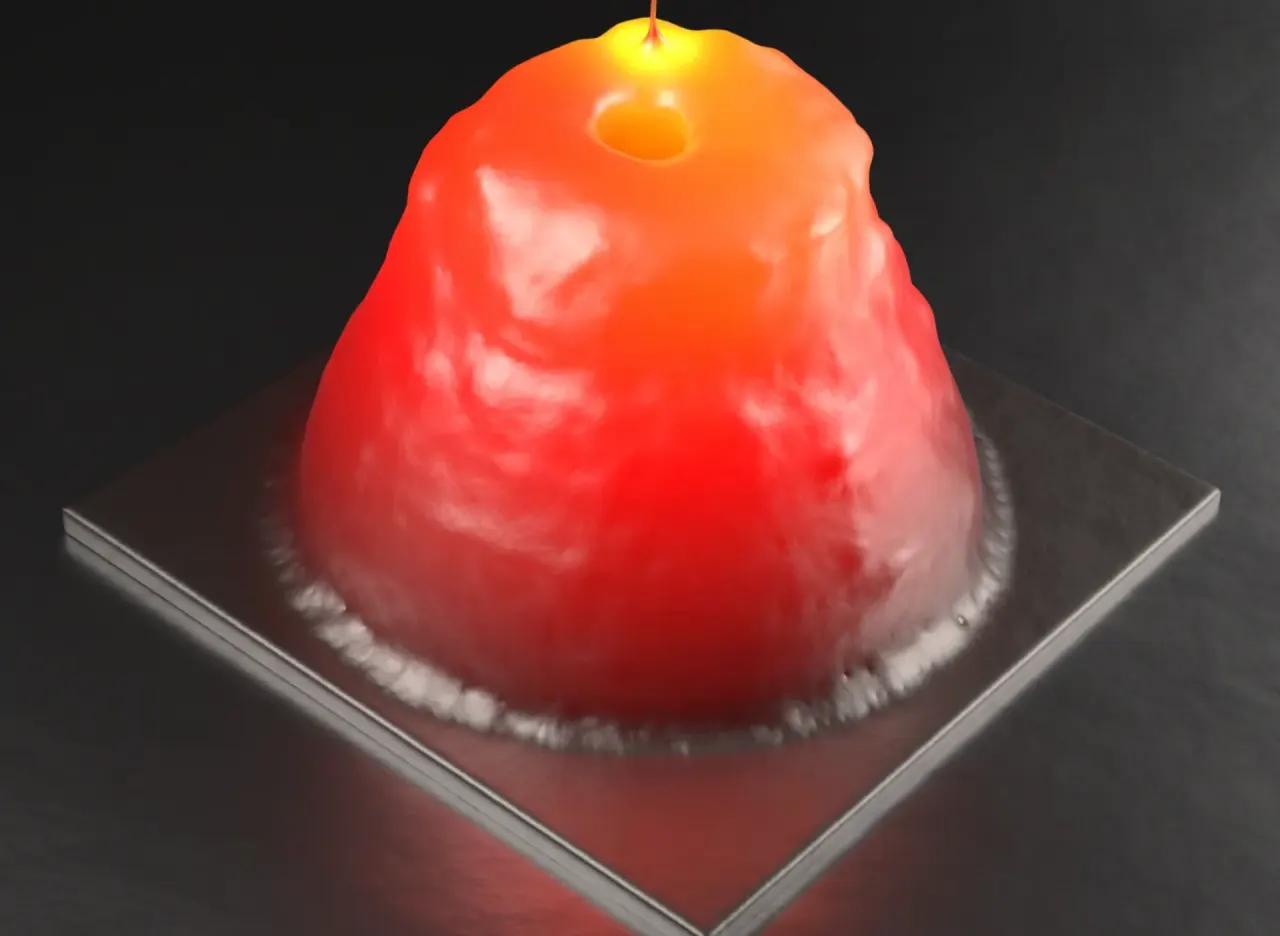
  2. Thin wall, many layersRunValues for this run only

    Simulation, demonstrator cone

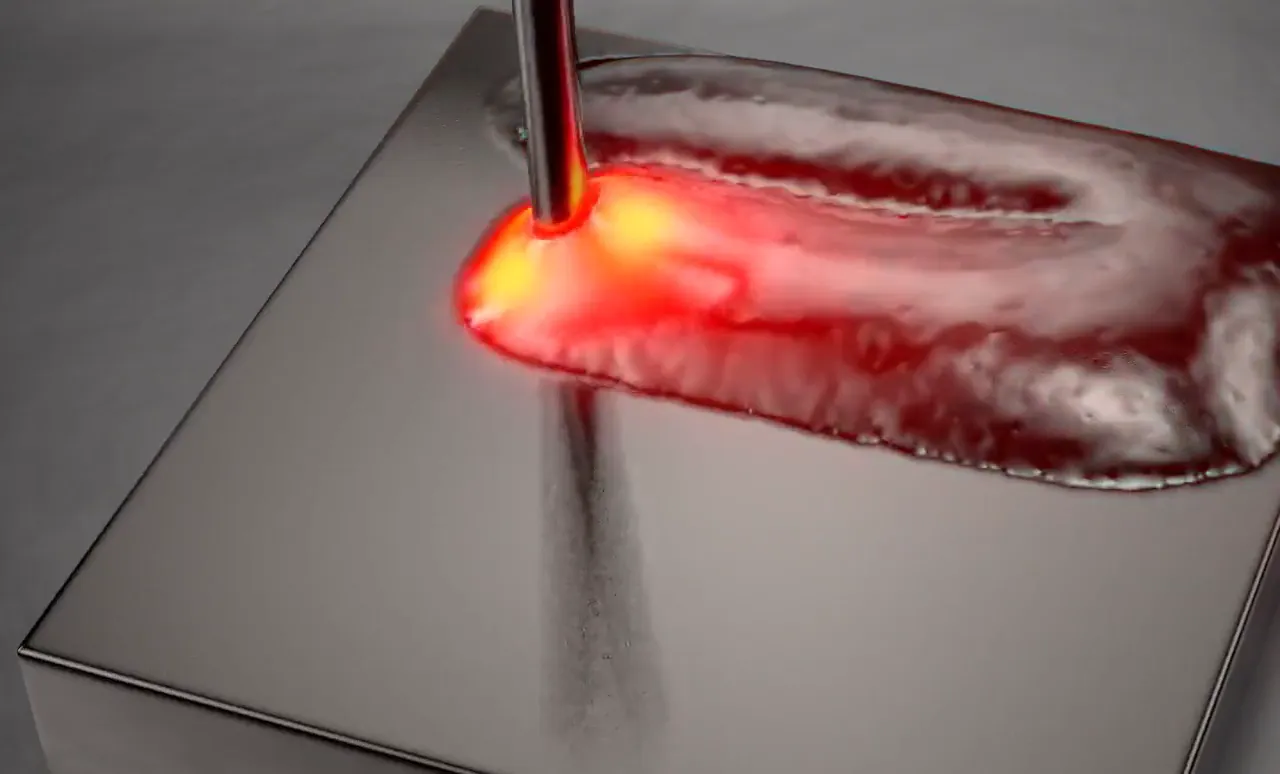
  3. CoatingRunRun shows the first layer only

    Simulation, demonstrator

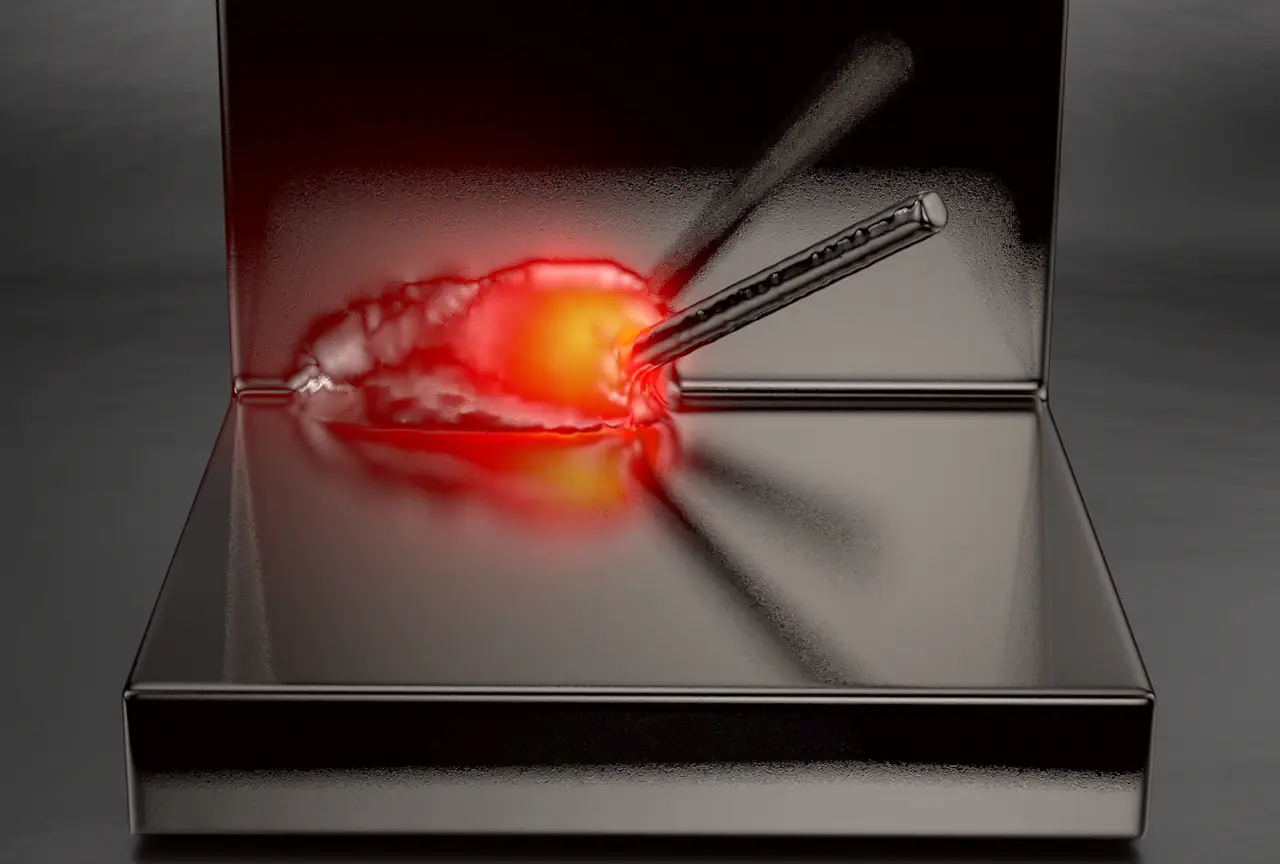
  4. Build-up on an existing partRunRun shows one bead only

    Simulation, demonstrator

  5. Overhangs, inclined wallsRunRun shows the overhead bead only

    Simulation, demonstrator

  6. RepairSchematic

    Schematic, illustration

Parameter finding today

Laser DED parameters are still determined in elaborate physical prints, for each material and each geometry. We set machine, material, geometry and toolpath for each enquiry.

New part

The software computes the parameters for a new geometry.

Because the layer height drifts with a fixed parameter set, the software adjusts the parameter set layer by layer.
Cube demonstrator, fixed parameter set
Cube demonstrator, adjusted parameter set

The overhang on the right comes from the undersized base plate in the model and is not a process defect.

One parameter set for all layers compared with adjusted parameters
What changesOne parameter setAdjusted parameters
Laser powerone value for all layersadjusted layer by layer
Travel speedone value for all layersadjusted layer by layer
Material feedone value for all layersadjusted layer by layer
Layer heightdriftsstays constant

Thin wall, many layers

The software computes parameters for a wall of many layers in which heat accumulates.

Goal: constant layer height over 40 minutes of build time.

Laser power640–1620W6001,2001,8006401620decreases as the part heats upWire feed5.8–12.6mm/s510155.812.6rises because the accumulated heatcan melt more wire010203040 minLaser power640–1620Wdecreases as the part heats up6001,2001,8006401620Wire feed5.8–12.6mm/srises because the accumulated heatcan melt more wire510155.812.602040 minLaser power640–1620W6001,2001,8006401620Wire feed5.8–12.6mm/s510155.812.602040 min

Laser power stays between 640 and 1620 W over 40 minutes and decreases as the part heats up. Wire feed stays between 5.8 and 12.6 mm/s and rises because the accumulated heat can melt more wire.

Cone demonstrator, wire: clip and curves from the same run

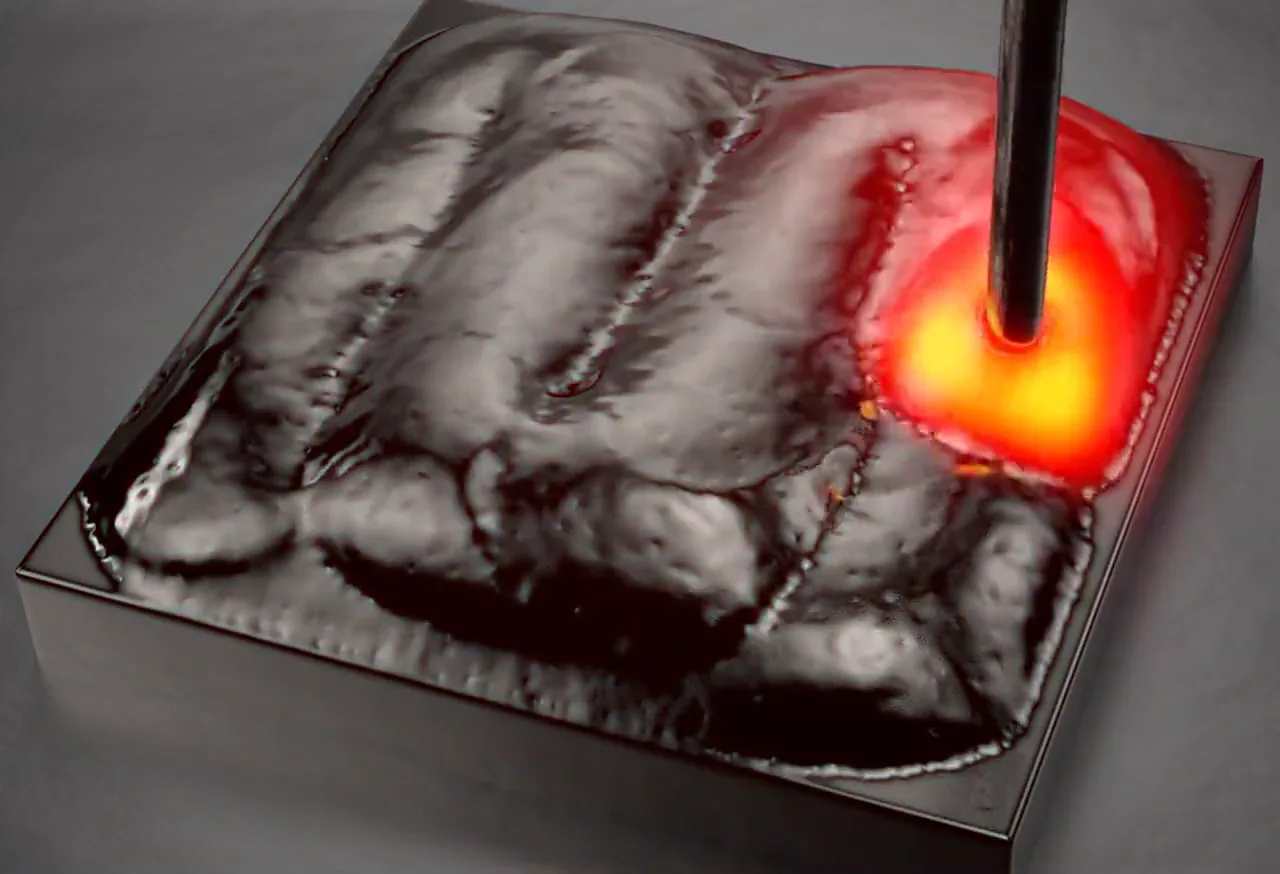
Coating

The software computes parameters for a functional layer deposited across the surface, bead beside bead.

With wire

Beads side by side on a plate

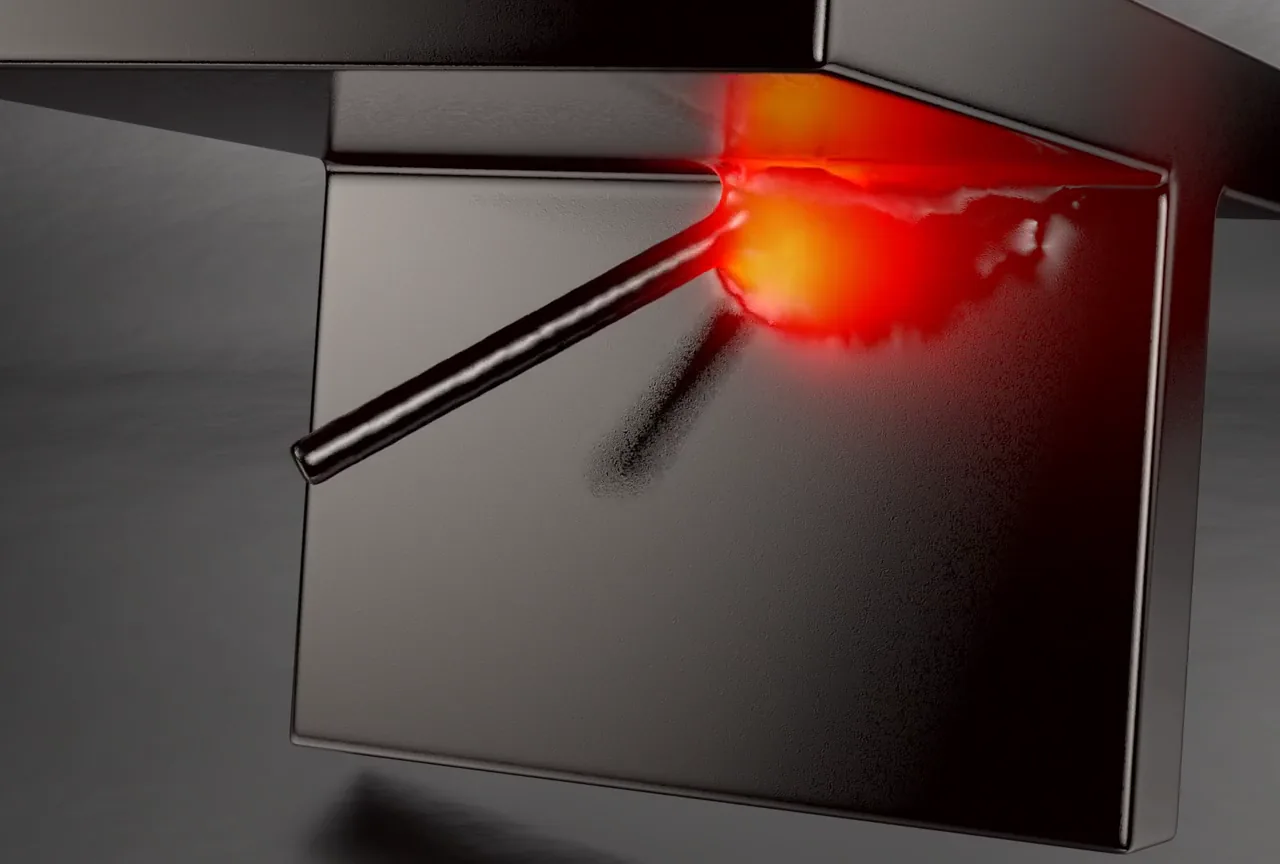
Build-up on an existing part

The software computes parameters for new geometry built up on an existing part.

With wire

A bead in the inner corner of an existing angle part

Overhangs, inclined walls

The software computes parameters for overhangs and inclined walls in which each layer is offset sideways.

With wire

A bead deposited overhead under a horizontal plate

Repair

The software computes parameters to rebuild a worn contour on the part.

Repair, schematicSection through a part with a worn edge. Two beads fill the notch layer by layer, a third is being deposited. Dashed: the original contour.

Schematic, illustration

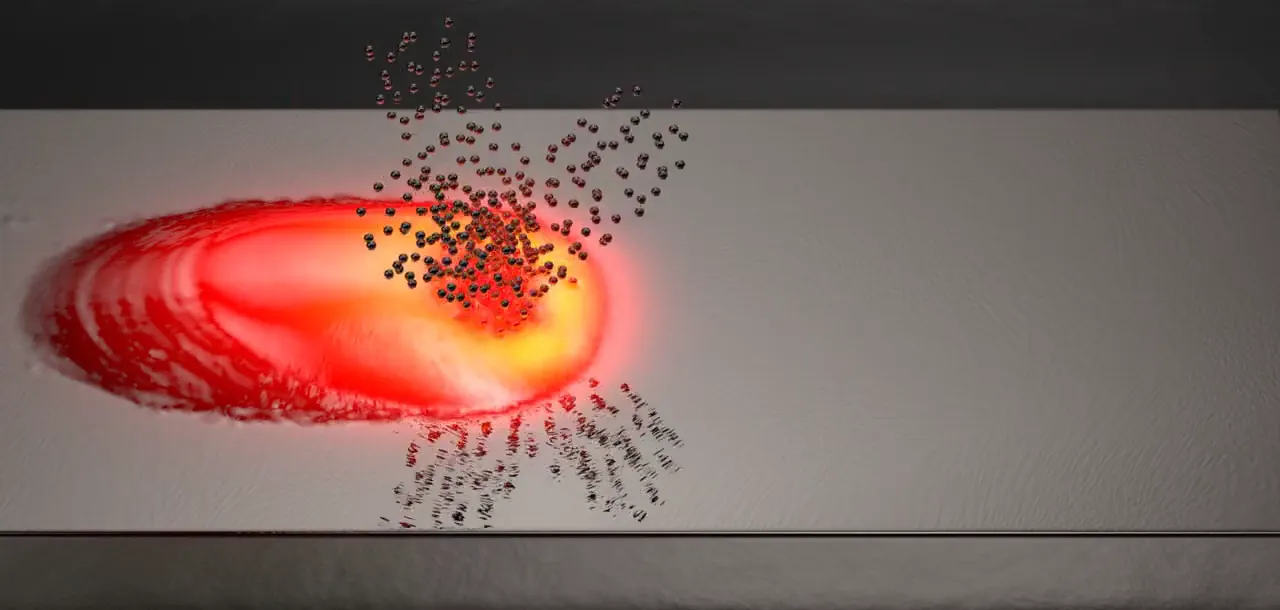
Deposition onto an existing part, schematic
Wire feed, a single bead
Powder feed, a single bead

Wire or powder

For each application the software simulates the process with wire or with powder.

Limits of the model

The simulation computes possible parameters for your geometry and your material. It does not replace the print.

Schematic, illustration

We simulate

Adjusted machine file (G‑code)

With a measurement
Calibrated with your measured bead, for example a cross-section.
Without a measurement
An exploratory study with simulated trends, without a calibrated comparison.

Handover

Your team

runs
the print on your machine.

Your team receives the machine file with adjusted process parameters, checks it before the print and uses it for further process development.

Division of tasks per application, schematic

State of the evidence

matched
Pure titanium with single-track experiments, founder’s doctoral thesis, 2023 (external)

What we do not promise

  • The qualification of your part.
  • A calibrated comparison without a measurement.
  • Savings as a result. Build time, energy or the number of prints are not a contractual result.

Let’s talk about your part

In a call we clarify whether the simulation answers your parameter question.

Book a call

You pick the slot on book.synafloat.com.

Enquiry via the contact form

You talk to Dr. Michael BlankThe founder has researched particle-based melt-pool simulation since 2017 and earned his doctorate in the field.

Funding

EXIST – from science to business
Funded by the EXIST Business Start-up Grant at the FAPS institute of FAU, funding period 09/2025 to 08/2026.
FAU – Friedrich-Alexander-Universität Erlangen-NürnbergFAPS – Institute for Factory Automation and Production Systems, FAU

Partner: Friedrich-Alexander-Universität Erlangen-Nürnberg (FAU). Synafloat is a spin-off of FAU.

ESA BIC Northern Germany

Incubated at the ESA Business Incubation Centre in Bremen since November 2026.